If you run a manufacturing business properly, then you should constantly be resupplying inventory for your buyers, and the better inventroy your produce, the faster your suppliers will move it off the shelves, decreasing the number of days in your model. But here’s the catch: inventory management isn’t so simple; it doesn’t take an MBA from Wharton to be able to do it, but it does require a mastery of systems and logistics, and among the most important is the reorder formula. The reorder formula is the trigger that keeps inventory levels correct, inventory moving, and prevents overstocking. Therefore, it needs to be one of the most efficient parts of the overall workflow.
We’ve noticed how important the reorder point formula is here at Method, and since 2010, we have been helping manufacturers automate it or optimize it through our ultra-customizable systems.
What is the reorder point formula?
The reorder point formula is: Reorder Point = (Average daily usage × lead time in days) + safety stock
The reorder point formula means what it sounds like: it’s the point you get to in your inventory where you should begin to replenish your stock, usually by purchasing new stock. So, the reorder point is the trigger than replinishes your stock, and because it works mainly on the back of numbers and metrics, it’s something that can be automated and optimized.
When dealing with the reorder point formula, two concepts need to be embraced.
- Average demand lead time: how much you’ll use while you wait for replenishment.
- Variability buffer: extra inventory (safety stock) to cover demand spikes or lead time delays.
The reorder point formula combines lead time demand (average usage during waiting period) with a variability buffer (safety stock) to provide for timely reordering prior to inventory exhaustion, regardless of potential spikes in demand or shipping delays. Because of this, the lead time demand accounts for “normal usage while waiting,” and safety stock is used to provide a buffer in case of adverse events. Let’s say a shop uses 20 units of a given part per day, and it usually takes 7 days for the supplier to deliver it. Here is how that’s expressed:
| Component | Calculation | Solution |
|---|---|---|
| Lead time demand | 20 × 7 | 140 units |
| Safety stock (buffer) | set buffer amount | 30 units (for spikes or delays) |
| Reorder point | 140 + 30 | 170 units |
Why reorder point essential in inventory management
It’s not too hard to imagine why an accurate reorder point might be essential, other than increasing efficiency and decreasing carrying costs. Rule number 1 of capitalism is to never run out of your product or service. The real issue is how you use the reorder point. Done efficiently and with the correct data, clients can see serious jumps in cost efficiency, which looks very good in their P&Ls.
Preventing stockouts and lost sales
No e-commerce company wants to sit there empty-handed when customers are knocking at the door (or clicking) . A re-order point that’s done correctly can keep shops full of stock, yet not enough to be sitting on too much at one time. Stockouts can cause problems all across the manufacturing chain, as missing parts lead to missed production, which leads to more issues in the supply chain.
Supporting replenishment planning
Replenishment planning should not be focused on above all on cadence, not necessarily perfection, related to the exact amount. There needs to be a rhythmic order for all parties involved in purchasing/receiving/production and customer delivery for everyone to follow. The use of reorder points provides the purchasing/planning teams with clear, reliable, and repetitive data that can be harnessed for automation.
Driving better service levels and fewer disruptions
Customer demand and customer satisfaction are intrinsically interlinked across the supply chain. If you are building lawnmower parts, and your supplier in Guiyang is always on time, then you are probably going to continue to shift business to that supplier, however, if that supplier has problems with their own inventory, this could cause problems for you and your clients. Hence, when dealing with manufacturing and supply chain, the domino effect is very real, and thus having your reorder point optimized is extremely important.
Method allows you to always be a great domino in the supply chain byconnecting your inventory, your sales activity, and purchasing activities within a single application, rather than being fragmented throughout multiple spreadsheets and email boxes. Through two-way synchronization with QuickBooks and custom workflows, teams can expedite reorder processes, decrease manual verification processes, and proactively prevent stockouts from becoming fires. The result is less hasty ordering, fewer missed shipments, and greater control over how much of your working capital is tied up at all times as inventory.
Key components of the reorder point formula
The reorder point formula consists of several data points. Below are some things to consider.
Lead time
Lead time is the maximum lead time between placing a replenishment order and having the inventory available for use. Depending on your environment, lead time may include:
| Lead time component | What it includes |
|---|---|
| Supplier production time | The time the supplier needs to manufacture, pick, or prepare the order after it is placed. |
| Transit time | Shipping time from the supplier to your facility, including carrier delays or customs clearance if applicable. |
| Receiving and inspection | Time required to receive, inspect, and verify quantities and quality upon arrival. |
| Put-away and system availability | Time until inventory is stored, recorded, and available for use in production or fulfillment. |
Two lead time concepts matter:
- Average lead time: your typical wait time.
- Lead time variability: how often lead time is longer or shorter than average.
For example, let’s say we have a lawnmower parts manufacturer located in Da Nang, Vietnam, and they normally experience a lead time of about 8 days from when they place a purchase order with their suppliers until they receive all of the required parts at the right time. However, their lead times can vary based upon a variety of factors, including supplier scheduling, shipping, or the amount of time that is needed to physically receive the parts and components necessary for completion.
In this example, if the factory produces and consumes 120 units of product per day and they experience a 3-day delay in receiving the parts necessary for manufacturing, they will need to produce at least 360 additional units of parts to cover the lost time and prevent their production schedule from being severely impacted. This then would require them to either create sufficient inventory to meet these needs or significantly alter the timing and sequence of their daily workflow.
Average lead time
| Lead time component | Days |
|---|---|
| Supplier production time | 4 |
| Transit time | 2 |
| Receiving and inspection | 1 |
| Put-away and system availability | 1 |
| Total lead time | 8 |
Lead time variability
| Lead time concept | Value |
|---|---|
| Average lead time | 8 days |
| Lead time variability | +0 to +3 days |
| Inventory usage rate | 120 units/day |
| Extra demand from a 3-day delay | 360 units |
Average daily usage or sales
Average Daily Usage is the average amount of inventory that a company normally uses within one day (or per week) during a normal day of operations. Average daily usage is more useful than sales many times, because consumption and production are tied together. As long as everything is stable, it’s pretty easy to calculate, and you can use a few different metrics,s such as SKU historical data, and shipment history. One thing to note here is that in the case of seasonal manufacturing, like lawn mowers and skiing, things can also be seasonal. In the lead time variability
Safety stock level
The safety stock calculation is extra inventory held as a buffer that hedges risk, and you can calculate safety stock using the following equation:
Safety stock = Z × σLT
Uncertainty in demand and lead time. Safety stock exists because real operations face variability in both demand and lead time. There are all sorts of reasons to require safety stock, whether it be to protect against climate risks, geopolitical risks, mutant viruses, and even extra terrestrial encountrs that could disrupt the supply chain.
Safety stock protects you when:
- Demand is higher than expected
- Lead time is longer than expected
- Both happen at the same time (this sucks )
Reorder point formula explained
As mentioned above, the reorder point is as follows:
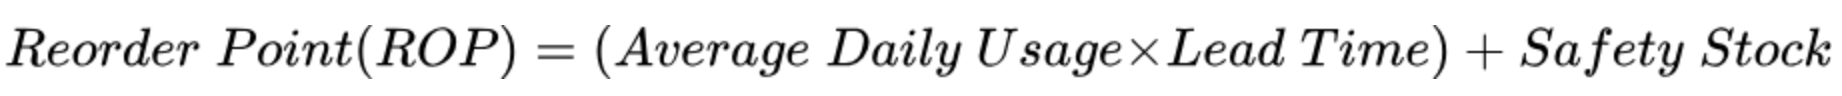
Why multiplying usage by lead time matters quite a lot
Any operation that burns 70 units (in this case) before the new order comes in should consider having some form of safety stock. This way, they can avoid running out of product if the order doesn’t arrive on time or if they have a higher-than-average number of orders during that period of time.
Step-by-step reorder point calculation example
Let’s walk through a manufacturing-friendly example using a single SKU.
Assume the following:
| Input | Value |
|---|---|
| Average daily usage | 12 units per day |
| Supplier lead time | 8 days |
| Safety stock target | 60 units |
Step 1: First step is to calculate lead time demand
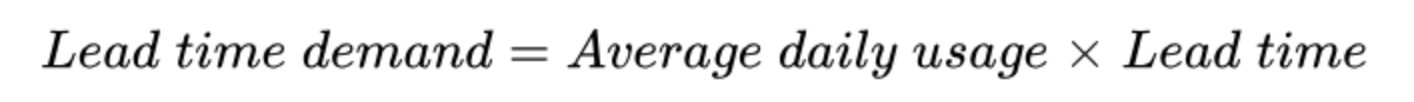
Lead time demand = 12 × 8 = 96 units
Step 2: Calculate the reorder point with no safety stock
ROP (no safety stock) = 96 units
If you reorder when inventory hits 96, then you are making the assumption that everything is happening as it should. That isn’t what happens in the real world, and thus, you need to calculate with safety stock.
Step 3: Calculate reorder point with safety stock
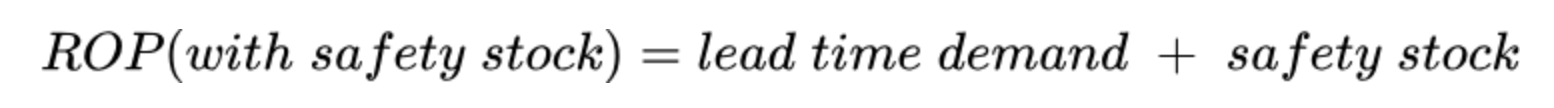
ROP = 96 + 60 = 156 units
Now your reorder point is 156. Now, you can implement a system in which once your inventory drops to 156, you can execute a task to reorder stock, and 60 units is your buffer.
What can change in real life when applied?
A lot can change in real life, such as lead times due to unforeseen tariffs or climate, which can result in running out of stock. These can quickly render a “correct” reorder point value obsolete, sometimes very shortly. A spreadsheet will keep using an outdated value until manually corrected, while a live system will continue to report current values based on what has happened.
Reorder point calculator tool
CALCULATOR?
Reorder point vs. reorder level
Reorder point is a mathematical equation as listed above, and although often used interchangeably with reorder level, the mathematical proofs are not the same. Reorder level is almost like managing your inventory on vibes; when you think the stock is low in your head, you order some more of it.
Reorder point in inventory management software
The great part of the re-order point is ithat t’s a mathematical equation that’s fed by data. Meaning that, in order to properly plan your reorder point, you need lots and lots of precise data, and this is where technology enters the fray. With Method, you can ditch the manual spreadsheets that are giving you inaccurate reorder points and automate significant portions of this workflow.
Why real-time alerts matter for small manufacturers
Manufacturing doesn’t exist in another dimension with a different version of space-time principles; it exists right here in this dimension and exists in real-time. If you are going to be using real-time to manufacture, your data better be real-time too, as it allows you to spot bottlenecks and problems before they happen. Method gives you your most important data in real time with state-of-the-art virtual dashboards.
Integrating reorder point with other inventory practices
Reorder point works best when it’s part of a broader inventory strategy. Two practices commonly pair well with it: EOQ and forecasting.
EOQ and reorder point
Reorder point and economic order quantity (EOQ) provide a business with a way to balance its inventory cost for purchasing products, as well as its inventory cost for carrying them. The combination of both is an effective method of creating a basic replenishment system: the reorder point will determine when to make the purchase, and the EOQ will determine the size of the purchase.
Forecasting and reorder point
The main point of forecasting a reorder point is to account for variations in demand. Demand doesn’t always remain flat, and especially due to seasonal or tarfiff related vulnerablities. Therefore, a reorder point sometimes needs to be forecasted. This can be done by playing around with the differnet metrics such as daily usage or safety stock.
Common mistakes and how to avoid them
Most reorder point failures are not math failures. They are operational failures: the inputs get stale, the team loses trust, and the signal stops driving action.
Relying on averages hides risk.
Risk: Suppliers that typically have timely delivery can be at fault for stockout when they experience a delay in shipping, worse with seasonality.
Fix: Build safety stock based on the real variability of the supplier’s lead time, particularly for important products.
Usage patterns shift faster than expected.
Risk: The addition of new customers, changes to the product mix, and the churning of schedules will rapidly age reorder points.
Fix: Update your reorder points with some frequency and review high velocity skus more frequently.
Gut feel creates inconsistency.
Risk: Inconsistency leads to some items being over-buffed with inventory while other items have no protection.
Fix: Identify categories for your productsand establish service levels in accordance with that strategy.
Control loops break without follow-through.
Risk: f control loops do not continue after initial implementation, no action occurs to adjust reorder points based on current transaction activity.
Fix: Connect triggers from reorder points to approvals, tasks, and workflows to make them visible and actionable.
These issues don’t arise from incorrect math; they arise from incorrect systems, data, and workflow.
Reorder point is pretty easy to master. Have you mastered it?
Reorder point is a mathematical equation, and at Method, we love mathematical equations, because that makes it easier to do our job, which makes it easier for you to do your job. The first step makes sure your data is accurate; real time visiblity into every nook and cranny of the factory floor is our specialty. Secondly, automate what you can! As long as you are harvesting the correct data, then you can automate part of the process. At Method, we specialize in taking your manufacturing process and melding our QuickBooks seamlessly, so that your reorder point is the best one in your niche.
FAQ
How does lead time affect reorder point?
The lead time will increase your reorder point (ROP) as you are now responsible for covering the usage of products while they are being delivered from the supplier. With an increase in lead times, your lead time demand (LTD) will also increase, and the ROP will also increase. In addition, if your lead time is variable, then your use of safety stock will become even more critical to ensure the continuity of your production process.
How often should the reorder point be recalculated?
First, you need to do proper demand forecasting before setting up your inventory management systems. Manufacturers generally recalculate their ROP at least once per month, but this may vary based on the volatility of demand and the reliability of suppliers. It would be beneficial to calculate the ROP at a greater frequency than this for products that move quickly through inventory and/or those whose failure to meet the ROP could result in serious consequences to the manufacturer’s production process and a delayed delivery time.
What if I don’t set my reorder point correctly?
Then all of your production line might become a mess. You should stop using an Excel spreadsheet and start using a proper CRM, like Method, to monitor average daily sales and inventory control.
Leave a Reply