In the world of manufacturing, margins are incredibly important, and there is nothing better than increasing margins with incremental improvements in efficiency. One of the best and easiest ways to accomplish this is to ensure your equipment is operating at peak performance through overall equipment effectiveness (OEE). OEE is an important equation, and an OEE calculator helps translate raw production data into a clear performance score.
Here at Method CRM, we’ve been supporting QuickBooks-based businesses since 2010. Method has become a favorite among business owners for providing two-way QuickBooks integration, customizations, and end-to-end sales automation. Below, we will provide information on how OEE works and how you can calculate OEE step by step. We will also show you the benefits of having accurate production data, which will enhance your team’s ability to operate effectively and make better decisions that drive higher profit margins.
What is overall equipment effectiveness (OEE)?
Overall Equipment Effectiveness (OEE) is an equipment and manufacturing efficiency metric that compares actual production equipment operating time to the theoretical maximum possible production time. OEE is used as a measure of how effectively productive time is utilized relative to planned productive time during production.
The three components of OEE
- Availability — how much of the planned production time is the equipment actually running
- Performance — how quickly the equipment runs compared to its ideal cycle time
- Quality — the percentage of good parts produced compared to total parts produced
These three elements serve as a holistic evaluation of the manufacturing process’s performance. Rather than examining individual areas such as unplanned downtime, lost time due to reduced speeds, and/or poor-quality products separately, the overall performance of the manufacturing process can be evaluated through a single score, OEE, which represents the operational efficiency of the process.
OEE formula explained step by step
The OEE formula breaks production performance into several measurable components.
Planned production time
Planned production time represents the total amount of time equipment is scheduled to run during a shift. This is different from the total shift length because some time may already be reserved for planned breaks or scheduled maintenance. Take an eight-hour shift, that’s 480 minutes. Subtract 60 minutes for breaks or scheduled shutdowns, and you’re left with 420 minutes of planned production time. This one’s pretty easy.
| Shift Length (Minutes) | Planned Breaks or Shutdowns (Minutes) | Planned Production Time (Minutes) |
|---|---|---|
| 480 | 60 | 420 |
Downtime
Downtime is the time a machine spends idle while it should be producing product. There are two types of downtime: planned and unplanned. Planned downtime can include, but is not limited to, maintenance scheduling, equipment changeovers, equipment inspection, etc. Unplanned downtime can include, but is not limited to, operator errors, machine breakdown, etc.
To illustrate this point, assume that you have 8 hours available in a workday and each hour has 60 minutes. Since there are 2 15-minute breaks and 1 30-minute break throughout the day, the total planned break/maintenance time is 1 hour. Therefore, the total number of planned production minutes would be 480 − 60 = 420. If we were to experience 1 additional hour of downtime during the same planned production time, our runtime would be 360 minutes, resulting in an availability rate of approximately 85.7% (360 ÷ 420).
| Step | Calculation | Result |
|---|---|---|
| Planned production time | 8 × 60 − 60 | 420 minutes |
| Downtime | — | 60 minutes |
| Run time | 420 − 60 | 360 minutes |
| Availability | 360 ÷ 420 | 85.7% |
Run time and operating time
Run time is the time the machine is running and producing product. To calculate runtime, first determine the downtime and subtract it from the planned production time, often referred to as “operating time.” In a typical OEE calculation, operating time is synonymous with run time. The runtime represents the actual time frame during which productive work takes place. An example of how this is modeled out is provided below.
| Step | Calculation | Result |
|---|---|---|
| Planned production time | — | 420 minutes |
| Downtime | — | 45 minutes |
| Run time | 420 − 45 | 375 minutes |
Ideal cycle time
The “ideal cycle time” represents the time a single person would require to produce a single unit of product at their highest level of performance; therefore, the ideal cycle time may serve as a point of comparison to determine how much actual production time can be lost within an operation. For example, if a machine can produce one unit in 30 seconds but is actually averaging one unit every 45 seconds, there is clearly a loss of productivity in the manufacturing process.
| Step | Calculation | Result |
|---|---|---|
| Ideal Cycle Time | — | 30 seconds per unit |
| Actual Cycle Time | — | 45 seconds per unit |
| Productivity Loss | 45 − 30 | 15 seconds |
Total count vs good count
OEE calculations distinguish between the total units produced and the units that meet quality standards.
- Total count — all parts or units produced during the run time
- Good count — units that meet quality standards without rework
For example, the table below shows how you can differentiate between these two.
| Step | Calculation | Result |
|---|---|---|
| Total Units Produced | — | 1,000 units |
| Defective or Reworked Units | — | 120 units |
| Good Units | 1,000 − 120 | 880 units |
Full OEE formula
The complete OEE calculation combines the three components:
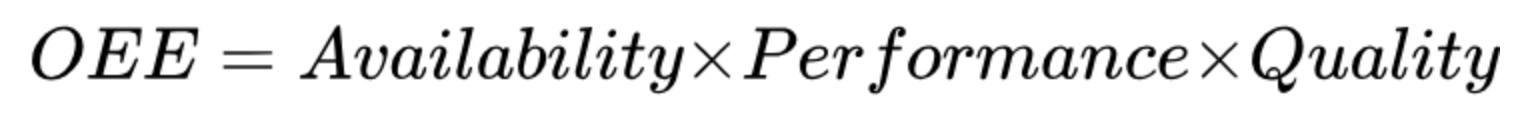
Each factor is calculated as follows:
| Component | Formula |
|---|---|
| Availability | Run Time / Planned Production Time |
| Performance | (Ideal Cycle Time × Total Count) / Run Time |
| Quality | Good Count / Total Count |
OEE calculator
Use the calculator below to estimate overall equipment effectiveness based on your production data. Enter planned production time, downtime, ideal cycle time, and production counts to generate an OEE score.
OEE Calculator
The interactive calculator will be embedded here.
OEE calculator example (with numbers)
It is helpful to go through an example of a production shift and calculate an overall equipment effectiveness (OEE) calculator by applying actual production numbers to the OEE equation; for instance, planned production time, total downtime, total units produced, and good units. Once this is done, it will be apparent how each of these categories contributes to the total OEE.
The OEE example shown here demonstrates how availability, performance, and quality are determined based on a single eight-hour production shift. Using the same type of calculations that OEE uses allows production staff to determine the areas of loss, either due to downtime, longer cycle times, or defective products.
Using these numbers, we can calculate each component:
| OEE component | Calculation | Result |
|---|---|---|
| Availability | Run time / Planned production time 390 / 420 |
92.8% |
| Performance | Ideal cycle time × Total count / Run time | Determined by comparing actual cycle time to ideal cycle time |
| Quality | Good count / Total count 450 / 500 |
90% |
Multiplying these factors produces the final OEE score for the production line.
What is a good OEE score?
Manufacturing teams often compare their OEE scores against established standards to gauge how effectively their equipment operates relative to other manufacturers in the lean manufacturing and TPM arenas. These are helpful to teams when trying to make sense of their OEE scores and determine whether there is still room for improvement across their processes.
In many manufacturing studies, an OEE score of 85% or higher is recognized as “world-class” performance. In a world-class scenario, equipment would be operating with very little downtime, high production speeds, and a very low defect rate. Most facilities are operating at levels significantly below this benchmark as they work to improve reliability, reduce waste, and optimize their production workflow.
For many organizations, OEE is less about achieving a number and more about establishing a baseline and continually improving all aspects of availability, performance, and quality.
Most facilities begin by establishing a baseline score and then improving each component gradually.
Why your OEE values may be low
Low OEE values often indicate a loss of efficiency relative to an operation’s overall capacity during a manufacturing run. If any of your availability, performance, or quality data are running lower than anticipated, you likely have a loss occurring at some point in the production flow due to time spent on equipment.
Common causes include:
- Frequent equipment changeovers
- Hidden micro-stops or short interruptions
- Poor production data collection
- High defect or rework rates
- Limited process automation
How to use OEE data to optimize your production line
When used to drive operational improvement, OEE metrics are the most useful. Production teams can better understand where inefficiencies exist within their operation and identify which area(s) to focus on to achieve the largest gain in productivity through reviewing and analyzing the three key areas of OEE: availability, performance, and quality. Rather than speculating about potential problem areas throughout the production process, OEE establishes a methodical approach for identifying losses throughout the entire process.
For example, production teams can minimize downtime through improved maintenance schedules, maximize throughput by optimizing cycle time, and improve product quality by reducing defects or rework. This type of operational improvement is directly aligned with the organization’s ability to reduce material waste, promote sustainability, and ultimately maximize its overall efficiency as a producer.
Manual OEE tracking vs automated systems
Many teams begin tracking OEE using spreadsheets or manual data collection. While this approach can provide initial insights, it introduces several challenges.
- Delayed reporting
- Human error in data entry
- Lack of real-time performance visibility
- Difficulty connecting production data to operational systems
Method CRM provides operational integrity through centralized business information and workflow integration of both upstream and downstream processes. Although Method is not a Manufacturing Execution System (MES), it enables the flow of clean operational data from quoting and production scheduling to the accounting systems, such as QuickBooks.
How better data improves profitability
Increasing Overall Equipment Effectiveness (OEE) is not just about improving machine productivity; it directly impacts the profitability of the entire organization. The additional productive output per unit of existing resources increases with consistent equipment operation and reduced production losses.
Increased OEE results in increased throughput, improved sustainability through decreased material loss and reduced energy consumption, and increased margins through decreased defect rates, resulting in less scrap and rework, and faster cycle times, resulting in increased reliability of delivery to customers. Having complete visibility into the current operational status of your production line, enabled by accurate, integrated operational data across systems, will enable you to quickly identify inefficiencies and continually improve your production line performance.
Understand your OEE; understand your operation
Everyone knows that the margins and manufacturing can be small, and in some cases, razor-thin. Any data that you can use to your advantage can help you win those pricing battles where decisions about product orders are made on the tiniest of margins. OEE can be one of the most important weapons in your arsenal, as it acts as a gauge of how well your equipment is doing on the floor, not just in theory.
It is through improved process performance and greater data accuracy that you will see the best performance improvements. Data is what’s powering the 21st century, and your CRM needs to be able to both store and leverage all that data so you can easily access and process it. This is where Method CRM shines; by connecting customer data, job information, and operational workflows with your financial systems, it gives manufacturers a clear view of how work moves from quote to production to invoicing. That visibility helps teams spot inefficiencies faster, track performance more accurately, and make better decisions about pricing, production, and capacity.
FAQ
How do you calculate overall equipment effectiveness?
To compute overall equipment effectiveness (OEE), three factors are multiplied together as follows: Availability x Performance x Quality. These three metrics each measure a different part of your production process efficiency.
What is considered a good OEE score?
Most of the time, 85% is often considered the best of the best when it comes to OEE performance. However, many manufacturing facilities operate between 60% and 75% until they can improve their internal operations.
What data is required for an OEE calculation?
Key data inputs include planned production time, downtime, ideal cycle time, total units produced, and the number of good units produced.
Leave a Reply